Choosing cutting data is not a matter of copying one chart and pressing “cycle start.” The practical question is how to select cutting parameters for different metals while protecting the tool, workpiece, and machine. Steel, aluminum, cast iron, titanium, and nickel alloys respond differently under the same cutter. Their hardness, thermal conductivity, toughness, and tendency to work-harden can change cutting behavior within seconds.
The scale of this challenge is substantial. The World Steel Association reported approximately 1.89 billion tonnes of crude steel production worldwide in 2023. That figure represents many grades, not one uniform material. Sandvik Coromant’s metal-cutting guidance also emphasizes that cutting speed, feed, and depth of cut must match the workpiece grade, tool material, and machining operation. ISO 3685 provides standardized methods for evaluating tool life during turning tests. These references offer a reliable foundation, but they cannot replace controlled trials on a real machine.
A good starting point is the tool manufacturer’s recommended cutting range. Then adjust carefully. A sharp carbide insert may cut aluminum quickly, while titanium often needs lower speed, stable clamping, and generous coolant delivery. Watch the chips. Blue chips, built-up edges, vibration, or sudden insert wear are useful warnings. Small changes matter.
Real workshops are rarely perfect.
Machine rigidity, coolant pressure, tool overhang, and operator experience can shift the result. I have seen a theoretically efficient feed rate produce poor surfaces because the tool holder was too flexible. Therefore, parameter selection should combine published data, inspection records, and measured cutting performance. The best setting is not always the fastest one. It is the setting that delivers predictable tool life, acceptable surface finish, safe chip control, and repeatable production costs.
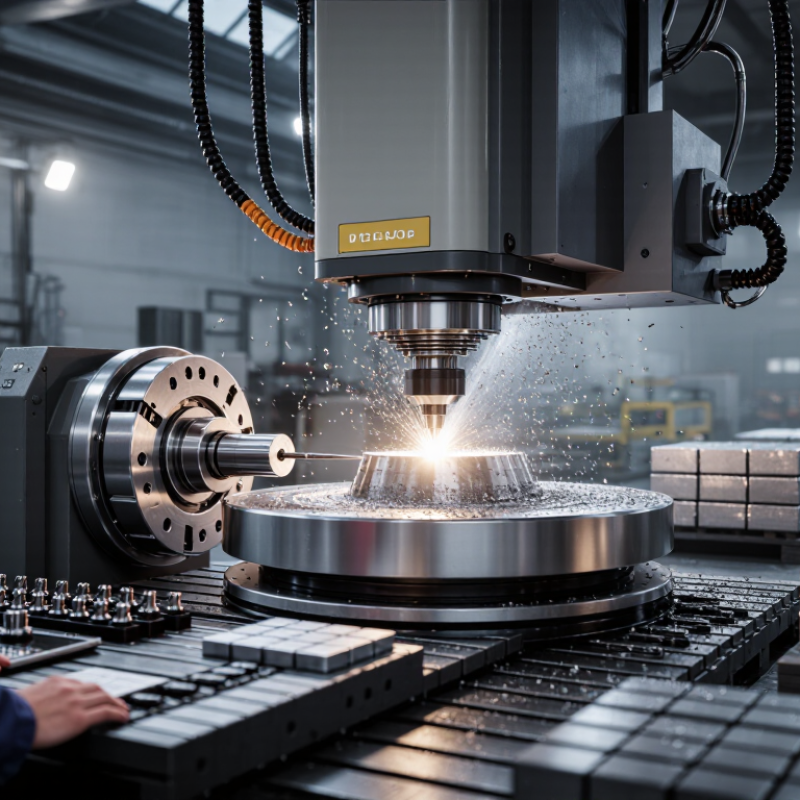
Metal properties directly influence cutting speed, feed rate, and depth of cut. Hardness resists tool penetration, while toughness can cause vibration and edge damage. Thermal conductivity matters too. Aluminum carries heat away quickly, but stainless steel often traps heat near the cutting zone. Heat tells a story.
A practical setup begins with the material certificate, tool geometry, and machine rigidity. For mild steel, moderate cutting speed and a steady feed usually produce a stable chip. Stainless steel may require a controlled feed to prevent work hardening. Titanium needs lower cutting speed because heat remains concentrated around the tool edge. Aluminum often accepts higher speed, but sharp geometry helps prevent built-up material.
Start conservatively. Watch chip color, sound, burr formation, and surface texture during the first pass. A blue chip can indicate excessive heat, while long, stringy chips may show poor chip control. Increase speed in small steps only after checking tool wear. Feed should create a formed chip, not dust or rubbing marks. Coolant can improve heat control, but it cannot correct an unsuitable parameter combination.
In shop trials, the strongest result often comes from balancing variables rather than maximizing one value. I have seen a slower cut produce better accuracy when the workpiece was thin or poorly supported. Parameter charts are useful, but they are not verdicts. Measure tool wear, part temperature, and dimensions after each adjustment. Even experienced operators sometimes overlook workholding stiffness.
Selecting cutting speed starts with the metal, but it should never end there.
These ranges are practical starting points, not fixed rules. Tool material, cutter diameter, machine rigidity, coolant, and depth of cut can change the result.
A 10 mm cutter at 100 m/min needs about 3,183 RPM. Check the machine limit before applying the number.
Watch the chips closely. Bright, well-formed chips often indicate stable cutting, while blue chips may signal excessive heat.
Stainless steel can work-harden when the tool rubs instead of cutting. Reduce speed slightly, maintain feed pressure, and avoid unnecessary pauses.
Aluminum may need a sharper edge and effective chip evacuation to prevent built-up material.
The first setting is rarely perfect. I have sometimes reduced speed by only 10 percent and gained a much cleaner surface. That small adjustment matters.
Listen for chatter, inspect the tool edge, and record the result for the next batch. A speed that works on one machine may fail on another, even with identical material.
How to Select Cutting Parameters for Different Metals?
Feed rate and depth of cut must match the metal, tool geometry, and machine rigidity. Feed rate is calculated as spindle speed × teeth × chip load. For aluminum, a starting chip load of 0.05–0.15 mm per tooth often suits small carbide cutters. Carbon steel commonly requires a lower range, around 0.03–0.10 mm per tooth. These figures align with cutting-data tables in the Machining Data Handbook, although actual results vary with tool diameter and coolant. Start conservatively.
Depth of cut controls cutting force and heat. A rigid machine may handle an axial depth near one tool diameter in aluminum. Steel often performs better near 0.25–0.50 times tool diameter. Stainless steel needs lighter engagement because heat stays near the cutting edge. Titanium needs even more restraint. The International Organization for Standardization’s ISO 3685 tool-life testing guidance emphasizes stable cutting conditions when comparing tool wear data. That matters in production.
Watch the chip, not only the display. A blue chip can signal excessive heat. A squealing tool may indicate weak workholding or excessive radial engagement. Reduce feed too much, and rubbing begins. I have seen operators blame the material when the real problem was a dull edge. Record spindle load, vibration, and edge wear after each trial. Adjust one variable at a time. Perfect settings rarely arrive immediately.
Starting feed rate and axial depth of cut for carbide end milling. Values assume a 10,000 RPM spindle and a 4-flute tool; actual settings should be adjusted for tool diameter, rigidity, coolant, and machine capability.
Feed rate: calculated as feed per tooth × number of flutes × spindle speed. Softer materials such as aluminum generally allow higher feed rates and deeper cuts, while stainless steel and titanium usually require more conservative settings to control heat and tool wear.
Selecting cutting parameters is not only about the metal. Tool material and machine condition often decide whether a cut remains stable. Start with the tool’s heat resistance, toughness, and edge geometry. A carbide tool can usually tolerate higher cutting speeds than high-speed steel, but it may chip under vibration. For hardened steel, reduce speed and cutting depth before increasing feed. For aluminum, a sharper edge and effective chip evacuation usually prevent built-up material.
Machine rigidity changes the safe working range. A heavy, well-aligned machine can handle deeper cuts and higher feed rates. An older machine may need smaller radial engagement, especially when spindle runout or backlash is present. Check the workholding carefully. A thin plate can sound quiet at low speed, then chatter suddenly. Reduce the overhang.
Keep coolant consistent.
Parameter changes should be gradual. After a test cut, inspect the chip shape, surface finish, tool edge, and spindle load. Blue chips may indicate excessive heat, while long, tangled chips can signal poor feed or chip control. I sometimes lower speed when the cutting data suggests an increase, because the machine’s vibration is more convincing than a chart. That judgment is not perfect. It should be recorded, tested, and reviewed. A stable process often comes from balancing tool limits with the machine’s real behavior, not its advertised capability.
Selecting cutting parameters for different metals should begin with a controlled test, not guesswork. Record the material grade, hardness, tool geometry, spindle speed, feed rate, and depth of cut. Use a small test piece first. Measure cutting temperature, surface roughness, chip shape, and tool wear after each pass.
Watch the process closely.
A steady sound often indicates stable cutting, while sudden vibration may signal excessive engagement or poor workholding. Long, tangled chips can suggest unsuitable feed or insufficient chip control. For aluminum, a sharp edge and effective chip evacuation are often important. Stainless steel may require lower heat input and steady feed pressure. Hardened steel usually demands reduced cutting depth and careful temperature control. These are useful starting points, not fixed rules.
Change one variable at a time whenever possible. A practical test may increase feed slightly while keeping speed and depth unchanged. Then compare tool wear and finished dimensions. I have sometimes blamed cutting speed for poor results when weak clamping caused the vibration. That mistake is easy to repeat. Check the setup before changing every parameter. Monitoring power demand, spindle load, and surface finish can reveal gradual problems before failure occurs. Stop the test if the tool chips, the workpiece moves, or heat becomes excessive. Keep clear records, including unexpected results. A parameter that performs well on one machine may behave differently after a tool change, coolant adjustment, or material batch variation.
Start with the metal, then consider tooling, machine rigidity, coolant, and cutting depth. These ranges are starting points, not fixed rules.
Aluminum often works around 150–400 m/min with carbide tooling. Use a sharp cutting edge and strong chip evacuation. Built-up material can damage the finish.
Mild steel commonly performs near 80–180 m/min. Stainless steel usually needs 40–100 m/min because heat builds quickly. Blue chips need attention.
Cast iron may tolerate about 60–140 m/min. Titanium often requires 25–60 m/min. Reduce heat and monitor tool wear closely.
Use RPM = 1,000 × cutting speed ÷ (π × tool diameter). A 10 mm cutter at 100 m/min needs about 3,183 RPM. Check the machine limit.
Bright, well-formed chips often suggest stable cutting. Blue chips may indicate excessive heat. Long, tangled chips can signal poor feed or chip control.
Sudden vibration may result from excessive engagement or weak workholding. Check clamping before changing every cutting parameter. Setup problems are easy to blame incorrectly.
Test a small workpiece first and record speed, feed, depth, temperature, finish, and tool wear. Change one variable at a time. Small adjustments matter.
Stop if the tool chips, the workpiece moves, or heat becomes excessive. Inspect the tool edge after each pass. Do not continue blindly.
Knowing how to select cutting parameters for different metals is essential for achieving accurate results, stable machining, and longer tool life. The process begins by evaluating each metal’s hardness, toughness, thermal conductivity, and tendency to generate heat or built-up edges. These properties guide the selection of cutting speed, while feed rate and depth of cut must be balanced according to the material, part geometry, tooling, and desired surface finish.
Cutting conditions should also be adjusted for tool material, machine rigidity, power capacity, workholding stability, and coolant availability. A practical approach is to begin with conservative settings, then monitor spindle load, vibration, chip shape, cutting temperature, tool wear, and surface quality. By making controlled adjustments and recording the results, operators can optimize performance, prevent premature tool failure, improve productivity, and maintain consistent quality across different metalworking applications.
Carto Tool