China Top 10 Tips to Improve Consistency in Batch Machining?

Time:2026-10-17 Author:Isabella
0%

Consistency is the quiet measure of machining excellence. In China’s competitive manufacturing sector, batch production must deliver repeatable dimensions, stable surface finishes, and predictable delivery times. A single worn insert can change a bore by several microns. That small shift may create assembly failures, rework, or customer complaints.

This guide examines how to improve consistency in batch machining through practical shop-floor controls. These include machine warm-up, tool-life monitoring, fixture verification, coolant management, statistical process control, and coordinate-measuring-machine inspection. Deloitte’s 2024 Smart Manufacturing and Operations Survey reported that 86% of manufacturing leaders expect smart manufacturing to become a major competitiveness driver within five years. However, digital tools cannot correct poor process discipline. ISO’s 2023 Survey also recorded more than 1.2 million ISO 9001 certificates worldwide, highlighting the continuing importance of documented quality systems.

W. Edwards Deming, a leading quality and manufacturing expert, stated, “Quality comes not from inspection, but from the improvement of the production process.” His point remains practical. Inspection finds variation after it appears. Better processes reduce variation before it spreads across a batch. Still, no checklist is perfect. A clean inspection report can hide inconsistent clamping pressure or an operator compensating manually. That is why this China-focused overview combines measurable controls with real production experience. The goal is not theoretical perfection. It is a more stable process, clearer evidence, and fewer surprises between the first part and the last.
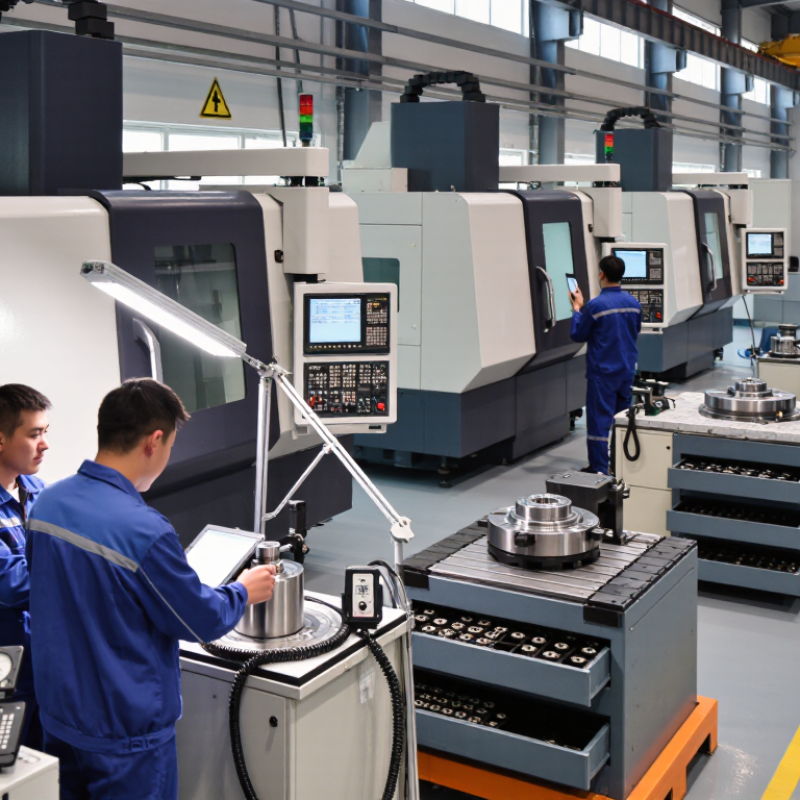
China Top 10 Tips to Improve Consistency in Batch Machining?

Set Batch Machining Targets: ISO 2768 Tolerances and Cpk ≥1.33

For batch machining in China, consistency starts with a clear tolerance plan. Use ISO 2768 tolerances for dimensions without individual specifications. However, do not apply general tolerances to critical fits or safety-related features. Those dimensions need direct requirements.

Tip 1: Define the target before production. Record the nominal size, tolerance class, material, machine, tooling, and inspection method. A drawing alone may not control process variation. Confirm the measurement equipment is calibrated and suitable for the tolerance. A loose fixture can create visible drift between early and late parts.

Tip 2: Track Cpk for important dimensions. A Cpk value of at least 1.33 indicates a capable, centered process under stable conditions. Collect data across several batches, not only from the first pieces. Check temperature, tool wear, coolant condition, and operator changes. A clean first-run report can still mislead. In practice, teams sometimes calculate Cpk from too few samples. That weakness deserves review. Use control charts and investigate trends before accepting the batch. If Cpk falls below 1.33, adjust the process rather than sorting defects repeatedly. Recheck the result after stabilization. Keep inspection records linked to batch numbers, machine settings, and corrective actions. This evidence supports reliable decisions and makes recurring variation easier to identify.

Stabilize CNC Processes: SPC at 3σ and First-Article Verification

Batch machining consistency starts with a stable CNC process, not final inspection. NIST/SEMATECH’s Statistical Methods Handbook states that three-sigma limits contain about 99.73% of normally distributed results. That figure sounds reassuring. It is not a quality guarantee. A process may stay within control limits while producing parts outside customer specifications.

Tip: Establish control charts for critical dimensions, tool wear, spindle load, and coolant temperature. Record measurements at fixed intervals. Operators should investigate unusual patterns before a dimension crosses its limit. On one production line, a slow bore drift appeared across twelve parts. The machine still passed inspection. The trend revealed a worn insert earlier.

First-article verification adds a physical checkpoint before batch production. Confirm the program version, fixture seating, tool offsets, material grade, datum structure, and measured features. Keep the inspection record with the job traveler. A 2023 global smart-manufacturing survey reported that 86% of manufacturers considered smart production important for competitiveness. Yet digital data is useless when setup records are incomplete. Our own weak point was trusting the first approved part too quickly. Rechecking only the obvious dimensions missed a burr near a mating surface. Use calibrated gauges, independent review, and traceable results. Three-sigma control plus disciplined first-article verification reduces variation, but it still demands human skepticism.

Control Machines and Tools: 20–22°C, Runout ≤0.01 mm, and Tool-Life Logs

Consistent batch machining starts with a stable environment, not just a capable operator. Keep the machine room between 20 and 22°C, and record temperature changes during each shift. A two-degree swing can alter workholding conditions, inspection results, and critical dimensions. Let the machine, fixtures, and material reach room temperature before cutting. This waiting period feels inefficient, but rushed setups often create hidden variation.

Check spindle, holder, and tool runout with a calibrated gauge. Keep total runout at or below 0.01 mm for sensitive operations. Measure near the cutting edge, where small errors become visible on the part. Clean the taper and contact surfaces before every setup. I once blamed insert wear for inconsistent bores, but dirt on the holder was the real cause. That mistake was avoidable. Still, it showed why records matter more than assumptions.

Create a tool-life log for every batch. Note tool number, material, cutting time, part count, coolant condition, and measured wear. Replace tools according to evidence, not habit alone. A tool may produce acceptable surfaces while dimensions slowly drift. Review the first, middle, and final parts from each run. Keep the samples. Compare them under the same measuring method. When results disagree, check the gauge, fixture pressure, and operator technique before changing cutting data. Small records build dependable decisions.

Validate Measurement Systems: GR&R <10% and Critical-Feature Inspection

In batch machining, consistency begins with a trustworthy measurement system. The AIAG Measurement Systems Analysis guideline classifies Gage R&R below 10% as generally acceptable, while 10% to 30% may require engineering review. Above 30% signals an unacceptable system. These limits are practical controls, not automatic guarantees. A low result cannot rescue a poorly designed fixture or an unstable operator method.

For a 25.00 mm bore with a ±0.02 mm tolerance, inspect the bore, gauge resolution, and temperature together. Use calibrated equipment with discrimination suitable for the tolerance. Many metrology teams apply a 10:1 resolution rule, also discussed in NIST measurement guidance. Repeat measurements across operators, shifts, and the full production range. Keep the raw readings. Averages can hide drift.

Critical-feature inspection should receive more attention than routine dimensions. Track bore size, true position, surface finish, and thread condition separately. In one practical review, repeated readings varied after operators changed clamping pressure. The gauge was not the only problem. The process was influencing the measurement. That finding required a revised fixture and clearer work instructions, not more inspection alone.

ISO 9001 quality principles support controlled monitoring, but they do not define one universal inspection frequency. Set sampling rates from risk, capability data, and customer requirements. Recheck GR&R after fixture changes, software updates, or unusual measurement trends. Small weaknesses matter.

Standardize China Shop-Floor Execution: 5S, SOPs, and OEE Above 85%

Consistency in batch machining starts with disciplined shop-floor execution. In a China machining shop, 5S should be visible at every workstation. Tools need marked locations, clean surfaces, and clear material zones. Operators should find gauges within seconds. Small delays often become large production losses.

SOPs must match real work, not office assumptions. Each document should show setup steps, fixture checks, tool offsets, inspection points, and approved responses to defects. A first-piece checklist can prevent an entire batch from drifting.

Supervisors should verify critical dimensions with calibrated instruments. Photos help, but they cannot replace practical training. Our early audits exposed an uncomfortable issue: some operators followed outdated instructions because nobody reviewed them.

OEE above 85% is a useful target, not a guarantee of quality. Track availability, performance, and quality by machine and shift. Record short stoppages, tool changes, waiting time, and rework. A clean dashboard can still hide weak data. Review the numbers daily with operators, then investigate recurring losses on the floor. Corrective actions should have owners and deadlines. Sometimes a simpler fixture or clearer inspection point improves consistency more than faster cutting. Reliable results come from repeating good habits, measuring honestly, and correcting imperfect systems.

FAQS

What room temperature supports consistent batch machining?

Keep the machining room between 20 and 22°C. Record temperature changes during every shift. Small swings can change dimensions and inspection results.

Why should machines, fixtures, and materials reach room temperature?

Temperature differences can affect workholding and critical dimensions. Let everything stabilize before cutting. Waiting feels inefficient, but rushed setups create hidden variation.

What runout limit is suitable for sensitive machining operations?

Keep total spindle, holder, and tool runout at or below 0.01 mm. Measure near the cutting edge. Clean tapers and contact surfaces before setup.

How can a tool-life log improve production decisions?

Record the tool number, material, cutting time, part count, coolant condition, and measured wear. Replace tools using evidence, not habit alone.

Can a tool produce acceptable parts while wearing out?

Yes. Surface finish may look acceptable while dimensions slowly drift. Check the first, middle, and final parts. Keep samples for comparison.

What should operators check when inspection results disagree?

Check the gauge, fixture pressure, and operator technique before changing cutting data. The gauge may be the problem. Records reduce guesswork.

What should a practical machining SOP include?

Include setup steps, fixture checks, tool offsets, inspection points, and approved defect responses. Add a first-piece checklist. Review instructions regularly.

How can 5S reduce delays at a workstation?

Mark tool locations, clean work surfaces, and separate material zones clearly. Operators should find gauges within seconds. Small delays accumulate quickly.

Is an OEE result above 85% enough to prove quality?

No. It is a useful target, not a quality guarantee. Track availability, performance, and quality by machine and shift.

What makes production improvement actions more effective?

Record short stoppages, tool changes, waiting time, and rework. Assign each action an owner and deadline. A simpler fixture may help more than faster cutting.

Conclusion

Improving consistency in batch machining requires a structured approach that combines clear targets, stable processes, reliable equipment, and disciplined shop-floor execution. Define acceptable dimensions using ISO 2768 tolerances and aim for a process capability index of Cpk ≥1.33. To understand how to improve consistency in batch machining, manufacturers should apply statistical process control with 3σ limits and verify the first article before full production. These steps help identify variation early and prevent defects from spreading across a batch.

Machine and tooling conditions should also remain controlled. Maintain the machining environment at 20–22°C, limit spindle or tool runout to 0.01 mm or less, and record tool life to support timely replacement. Measurement systems should be validated through GR&R studies, with results below 10%, while critical features receive focused inspection. Finally, 5S practices, standardized operating procedures, and an OEE target above 85% can improve organization, accountability, and repeatability throughout the production process.

Isabella

Isabella

Isabella is a dedicated marketing professional with a sharp focus on driving brand growth and engagement through strategic content creation. With an extensive background in digital marketing, she combines her passion for storytelling with her keen understanding of industry trends to deliver......